Inconel is a registered trademark originally developed by the International Nickel Company and now owned by Special Metals Corporation.
Inconel alloys occupy a unique position in modern engineering. They are not merely high-performance materials; they are enabling materials—metals that allow machines to operate in conditions where conventional steels would fail within hours.
From the combustion chambers of jet engines to the harsh interiors of chemical reactors, Inconel alloys deliver a combination of high-temperature strength, oxidation resistance, and corrosion resistance that few material families can match.
Investment casting is particularly important for complex Inconel components because it can produce near-net-shape geometries with internal passages, thin sections, curved profiles, and integrated structural features.
However, the process must be carefully adapted to the specific alloy because different Inconel grades have substantially different solidification and strengthening mechanisms.
1. What Is Inconel Alloy?
Inconel is a registered trademark associated with a family of nickel-based superalloys developed for demanding environments involving high temperature, oxidation, corrosion, pressure, and mechanical loading.
Although “Inconel” is technically a trademark rather than the name of a single alloy, the term is widely used in industry to describe nickel-chromium alloys such as Inconel 600, 601, 625, and 718, as well as several cast nickel-based superalloys.
The composition and strengthening mechanism vary significantly between grades, but most Inconel alloys contain a nickel-rich matrix,
with chromium and other alloying elements added to provide specific combinations of corrosion resistance, high-temperature strength, and metallurgical stability.
Typical nickel contents are approximately 50–75 wt.%, while chromium commonly falls in the range of 14–25 wt.%, depending on the grade.
Key Alloying Elements in Inconel
| Alloying Element | Typical Function |
| Nickel (Ni) | Forms the primary matrix and provides high-temperature stability and corrosion resistance |
| Chromium (Cr) | Improves oxidation resistance and resistance to high-temperature corrosion |
| Molybdenum (Mo) | Provides solid-solution strengthening and improves resistance to localized corrosion |
| Niobium (Nb) | Contributes to precipitation strengthening, particularly in Inconel 718 |
Aluminum (Al) |
Promotes formation of strengthening γ′ phases and improves oxidation resistance |
| Titanium (Ti) | Participates in γ′ precipitation strengthening |
| Iron (Fe) | Adjusts composition, phase stability, and manufacturing characteristics |
| Cobalt (Co) | Can improve high-temperature strength and phase stability in selected grades |
| Tungsten/Tantalum (W/Ta) | Provide additional high-temperature and solid-solution strengthening in certain superalloys |
Based on their strengthening mechanism, Inconel alloys can generally be divided into solid-solution-strengthened and precipitation-strengthened families.
Solid-solution grades such as Inconel 600 and 625 obtain much of their strength from alloying elements retained in the nickel matrix,
while precipitation-strengthened grades such as Inconel 718 develop higher strength through controlled formation of strengthening phases, particularly γ′ and γ″.
For casting applications, alloy selection is especially important because not every commercial Inconel grade is equally suited to foundry production.
Some grades are primarily developed as wrought alloys, whereas alloys such as Inconel 713C and 738 are specifically associated with cast nickel-based superalloy applications.
During casting, factors such as segregation, solidification behavior, shrinkage, hot cracking, and subsequent heat treatment must therefore be considered together with the required service temperature and mechanical properties.
Compared with conventional stainless steels, Inconel generally provides a higher level of high-temperature strength and oxidation resistance, particularly under severe thermal and corrosive conditions.
However, this performance comes with higher material cost and greater manufacturing difficulty, including more demanding melting, casting, machining, and heat-treatment requirements.
2. Chemical Composition of Common Inconel Alloys
The table below summarizes typical chemical compositions of selected Inconel grades.
Values are approximate and should be verified against the relevant ASTM, AMS, or UNS specification for a specific order.
| Alloy | UNS | Ni | Cr | Fe | Mo | Nb + Ta | Other |
| Inconel 600 | N06600 | ≥72.0 | 14.0–17.0 | 6.0–10.0 | — | — | Cu ≤0.5, C ≤0.15 |
| Inconel 601 | N06601 | 58.0–63.0 | 21.0–25.0 | Balance | — | — | Al 1.0–1.7 |
| Inconel 617 | N06617 | ≥44.5 | 20.0–24.0 | ≤3.0 | 8.0–10.0 | — | Co 10.0–15.0, Al 0.8–1.5 |
| Inconel 625 | N06625 | ≥58.0 | 20.0–23.0 | ≤5.0 | 8.0–10.0 | 3.15–4.15 | C ≤0.10 |
| Inconel 718 | N07718 | 50.0–55.0 | 17.0–21.0 | Balance | 2.8–3.3 | 4.75–5.50 | Ti 0.65–1.15, Al 0.20–0.80 |
| Inconel X-750 | N07750 | ≥70.0 | 14.0–17.0 | 5.0–9.0 | — | 0.70–1.20 | Ti 2.25–2.75, Al 0.40–1.00 |
| Inconel 738 | N07738 | Balance | 15.0–16.5 | ≤0.5 | 1.5–2.5 | Ta 1.5–2.5 | Co 8.0–9.0, Ti 3.0–4.0, Al 3.0–4.0 |
3. Key Properties of Inconel Alloys
Inconel alloys are selected for one or more of the following properties.
High-Temperature Strength
Inconel alloys retain useful strength at temperatures from 600°C to over 1000°C, depending on grade.
Precipitation-hardened grades such as 718 and 738 maintain high yield strength through the formation of coherent gamma-prime and gamma-double-prime precipitates.
Solid-solution grades such as 625 rely on molybdenum, niobium, and chromium to resist deformation.
Oxidation Resistance
Chromium forms a dense, adherent Cr₂O₃ scale that protects the underlying metal.
Inconel 601 and 617 are particularly resistant to cyclic oxidation and can operate in air at temperatures up to approximately 1200°C in some conditions.
Corrosion Resistance
Inconel alloys resist a wide range of corrosive media, including:
- Chloride-containing environments
- Seawater and marine atmospheres
- Acidic and alkaline solutions
- High-temperature sulfidation and carburization
- Molten salts and liquid metals
Inconel 625 is especially noted for resistance to pitting, crevice corrosion, and stress corrosion cracking in chloride environments.
Creep and Stress-Rupture Resistance
At high temperatures, metals deform slowly under constant load—a phenomenon known as creep.
Inconel alloys are engineered to resist creep through grain-boundary strengthening, solid-solution strengthening, and precipitation hardening. This makes them suitable for turbine blades, vanes, and high-pressure piping.
Fatigue Resistance
Thermal cycling and mechanical vibration are common in aerospace and power generation.
Inconel alloys exhibit good low-cycle and high-cycle fatigue resistance, particularly when produced with clean, defect-free microstructures.
Thermal Stability
Long-term exposure to elevated temperatures can cause phase transformations, embrittlement, or sigma-phase formation in some alloys.
Properly balanced Inconel grades resist these changes, maintaining ductility and toughness over thousands of hours.
Weldability and Machinability
Weldability varies by grade. Inconel 600, 625, and 718 are generally considered weldable using matching or nickel-based filler metals.
Machinability is generally poor compared with carbon steel or stainless steel, requiring sharp tooling, low speeds, and generous coolant.
4. Inconel Mechanical and Physical Properties
The following values are representative data for Inconel 625 in annealed or solution-treated wrought condition; actual properties vary with product form, section size, heat treatment, and test temperature.
These values should not be used as a substitute for the requirements of the applicable material specification.
| Property | Inconel 625 Typical / Reference Value |
| UNS Designation | N06625 |
| Werkstoff Number | 2.4856 |
| Nominal Alloy Type | Ni-Cr-Mo-Nb |
| Density | 8.44 g/cm³ |
| Melting Range | 1290–1350°C (2350–2460°F) |
| Young’s Modulus | ~207 GPa |
| Poisson’s Ratio | ~0.30–0.31 |
| Thermal Conductivity | ~9.8 W/m·K at 21°C |
| Specific Heat | ~410 J/kg·K |
| Coefficient of Thermal Expansion | ~12.8 × 10⁻⁶ /K, 21–93°C |
| Electrical Resistivity | ~1.29 × 10⁻⁶ Ω·m |
Tensile Strength |
~827–965 MPa, depending on condition/product |
| 0.2% Yield Strength | ~414–480 MPa, depending on condition/product |
| Elongation | Typically ≥30% in many annealed products |
| Hardness | Typically around 145–220 HB, condition-dependent |
| High-Temperature Strength | Retains substantial strength to roughly 815°C in suitable service |
| Oxidation Resistance | Good oxidation resistance up to approximately 980°C in appropriate environments |
| Magnetic Behavior | Generally very low magnetic permeability in annealed condition |
5. Why Use Inconel for Casting?
Casting is often the most practical and economical way to produce Inconel components. There are several reasons.
- Near-net shape: Casting minimizes machining, which is critical because Inconel is difficult to cut.
- Complex geometry: Internal cooling passages, thin walls, and intricate contours can be produced as one piece.
- Material utilization: Less scrap compared with forging or machining from bar stock.
- Alloy flexibility: Casting can produce alloys that are difficult or impossible to wrought, such as certain high-volume-fraction gamma-prime alloys.
- Directional and single-crystal structures: Advanced casting techniques can control grain structure for turbine blades, improving creep resistance.
- Repair and replacement: Cast components can often be repaired by welding or reconditioned, extending service life.
- Cost-effective for small and medium batches: Tooling costs can be amortized over production runs, making casting attractive for specialized parts.
6. Inconel Casting Processes
Different casting processes are suitable for different Inconel applications.
The appropriate process depends on the alloy grade, component size, wall thickness, internal geometry, dimensional requirements, production volume, and required material integrity.
Among the available methods, investment casting is generally the most important process for complex precision components.
Investment Casting
Investment casting, also known as lost-wax casting, is widely used to manufacture complex Inconel components with near-net-shape geometry.
The process begins with a wax pattern that reproduces the desired component geometry.
Multiple wax patterns may be assembled onto a runner system to form a casting tree, after which the assembly is repeatedly coated with ceramic slurry and refractory material to create a ceramic shell.
After the shell reaches the required thickness and strength, the wax is removed and the shell is fired. Molten Inconel is then poured into the heated ceramic mold.
After solidification, the shell is removed, the castings are cut from the tree, and subsequent operations such as grinding, heat treatment, CNC machining, and inspection are performed.
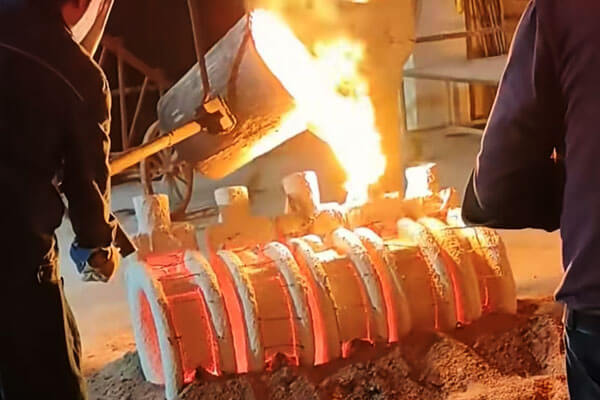
For Inconel components, investment casting offers several important advantages:
- Complex geometry: Internal passages, curved surfaces, ribs, bosses, and integrated features can often be incorporated directly into the casting.
- Near-net-shape production: Less machining stock is required than with conventional wrought-stock machining.
- Good dimensional reproducibility: Appropriate process control can provide consistent geometry across production batches.
- Material efficiency: This is particularly valuable for high-cost nickel-based alloys.
- Reduced assembly: Complex parts can often be produced as a single casting.
The gating and feeding system must be designed carefully because Inconel alloys can be sensitive to solidification shrinkage and hot cracking.
The thermal condition of the ceramic shell is also important because it influences filling behavior and solidification.
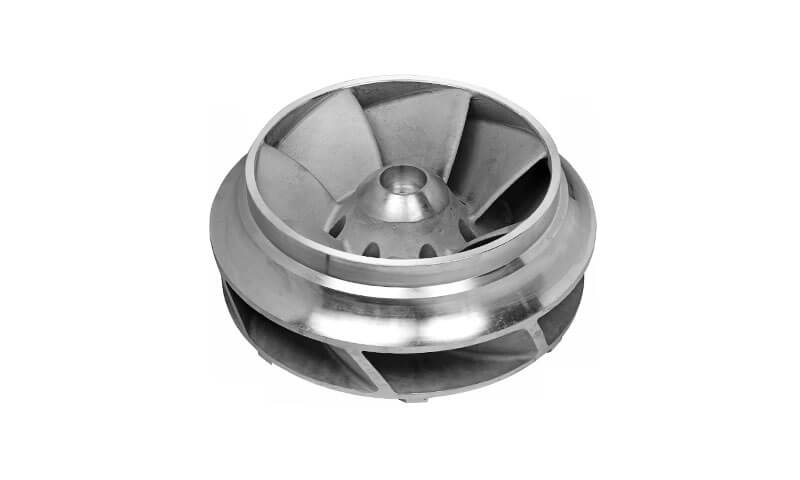
Investment casting is especially suitable for impellers, nozzles, turbine-related components, complex valve or pump components, heat-resistant housings, and other geometrically complex parts where material performance and dimensional precision are both important.
Vacuum Investment Casting
Vacuum investment casting combines the geometric advantages of investment casting with a controlled low-pressure environment during melting and/or pouring.
It is particularly valuable for high-performance nickel-based superalloys where control of gas contamination, oxidation, inclusions, and reactive alloying elements is important.
During vacuum melting, the furnace atmosphere is controlled to minimize unwanted reactions between the molten alloy and the surrounding environment.
The molten Inconel is then introduced into a ceramic investment mold under controlled conditions.
Vacuum processing can provide several metallurgical advantages:
- Reduced interaction with atmospheric gases
- Better control of oxidation-sensitive alloying elements
- Lower risk of certain gas-related defects
- Improved control of melt cleanliness
- Greater suitability for demanding aerospace, energy, and high-temperature components
The benefits depend strongly on furnace design, vacuum level, alloy chemistry, ceramic system, pouring practice, and process control.
Vacuum casting does not automatically eliminate defects; mold reactions, shrinkage, segregation, inclusions, and solidification-related defects still need to be controlled through proper engineering and inspection.
Vacuum investment casting is particularly appropriate for high-integrity, high-value Inconel castings where metallurgical quality is more important than minimizing initial process cost.
Centrifugal Casting
Centrifugal casting uses controlled rotational force to distribute molten metal against the mold wall during solidification.
The process is most suitable for components with cylindrical, annular, tubular, or rotationally symmetric geometries.
For suitable Inconel components, centrifugal casting can offer good feeding characteristics and may help reduce certain internal defects because denser molten metal is forced toward the outer region of the mold while some lighter inclusions or gases tend to migrate differently during solidification.
However, centrifugal casting is much less flexible than investment casting for highly complex three-dimensional geometries.
It is therefore generally selected according to component geometry rather than simply alloy preference.
Potential applications include:
- Rings and sleeves
- Cylindrical shells
- Tubular components
- Rotationally symmetric high-temperature parts
- Selected corrosion-resistant process components
Process parameters such as rotation speed, pouring temperature, mold temperature, wall thickness, and solidification rate must be controlled carefully.
Incorrect parameters can contribute to segregation, dimensional variation, inclusions, or undesirable microstructures.
For complex non-axisymmetric Inconel components, investment casting is usually more practical; for suitable rotational geometries, centrifugal casting can provide an efficient alternative.
Sand Casting
Sand casting uses a bonded sand mold to form the external geometry of the component.
Compared with investment casting, it generally offers greater flexibility for large components and relatively low production volumes, while requiring less expensive tooling.
For Inconel, however, sand casting presents additional challenges.
The mold surface, binder system, permeability, thermal behavior, pouring conditions, and metal-mold reaction must all be carefully controlled because nickel-based superalloys are sensitive to contamination and casting defects.
The main advantages of sand casting include:
- Lower tooling investment for large or low-volume components
- Ability to produce larger castings
- Flexible mold dimensions
- Practicality for certain prototypes, repair-related production, and specialized components
Its limitations are equally important. Compared with investment casting, sand casting generally provides lower surface quality, less precise dimensional reproduction, and greater machining requirements.
Complex thin-wall Inconel components are also more difficult to produce consistently.
For these reasons, sand casting is normally considered when component size, production volume, or tooling economics outweigh the need for very fine geometric detail.
For complex, high-value Inconel components requiring high dimensional accuracy and near-net-shape geometry, investment casting or vacuum investment casting is generally the more appropriate choice.
7. Surface Finishing and Post-Casting Treatment
Casting is only the beginning. Inconel castings require carefully controlled post-processing to achieve final properties and surface quality.
Heat Treatment
- Solution annealing – dissolves precipitates and homogenizes the microstructure.
- Aging – precipitates strengthening phases such as gamma-prime and gamma-double-prime.
- Stress relief – reduces residual stresses from casting and machining.
- HIP (Hot Isostatic Pressing) – applies high temperature and isostatic pressure to close internal porosity. HIP is often essential for fatigue-critical Inconel castings.
Surface Finishing
- Shot blasting – removes scale and improves surface cleanliness.
- Pickling and passivation – removes oxide scale and restores corrosion resistance.
- Machining – achieves critical dimensions, flange faces, and sealing surfaces.
- Grinding and polishing – improves surface finish for hygienic or aerodynamic requirements.
- Shot peening – induces compressive residual stresses to improve fatigue life.
- Coating – thermal barrier coatings or wear-resistant coatings may be applied.
Inspection and Testing
- Visual inspection
- Dimensional inspection
- Dye penetrant inspection (DPI)
- Radiographic inspection (X-ray)
- Ultrasonic inspection
- Chemical analysis
- Mechanical testing
- Pressure testing
A rigorous quality plan ensures that cast Inconel components meet the demanding requirements of aerospace, power generation, and chemical processing.
8. Applications of Cast Inconel Alloys
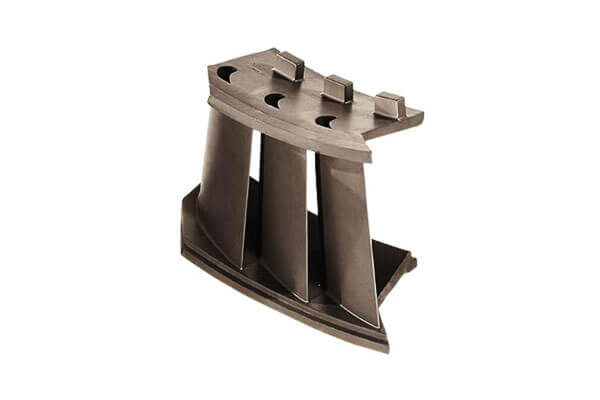
Turbine and High-Temperature Power Components
Cast nickel-based superalloys are widely associated with high-temperature rotating and stationary components.
Their ability to maintain strength and resist creep at elevated temperatures makes them suitable for demanding thermal environments.
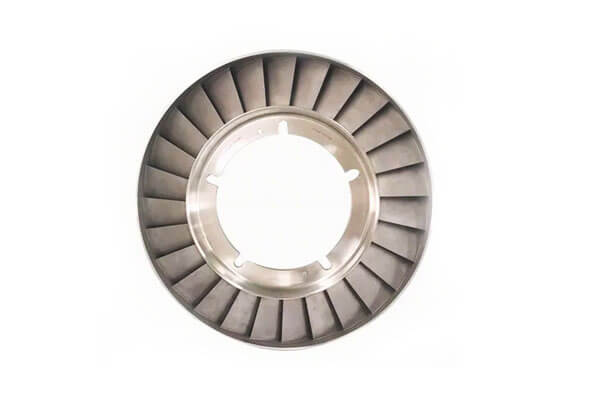
Typical applications include turbine-related housings, nozzle components, combustion components, heat-resistant structural parts, and other high-temperature gas-path hardware, depending on the specific alloy and design requirements.
Cast grades such as Inconel 713C and 738 are particularly relevant where elevated-temperature mechanical performance is a primary design requirement.
Chemical Processing Equipment
Inconel alloys are well suited to chemical environments where conventional stainless steels may experience excessive corrosion or loss of performance.
Cast components may include:
- Valve bodies and flow-control components
- Pump housings and impeller-related components
- Chemical processing housings
- Nozzles and fittings
- Heat-resistant process components
In applications involving chlorides, acids, or mixed chemical environments, alloy selection must be matched carefully to the actual process chemistry rather than relying solely on a general “corrosion-resistant” classification.
Oil and Gas Equipment
Oil and gas equipment may encounter combinations of high pressure, elevated temperature, chlorides, sour environments, and erosive fluids.
Inconel 625 and related nickel alloys are therefore used in selected components requiring high corrosion resistance and mechanical reliability.
Potential applications include valve and pump components, pressure-containing parts, subsea equipment, and specialized flow-control hardware.
Marine and Offshore Equipment
Seawater environments present significant corrosion challenges because of chloride exposure and localized corrosion mechanisms.
Suitable Inconel grades can provide strong resistance in marine environments, particularly where stainless steels or lower-alloy materials have insufficient resistance.
Cast components can be used in pumps, valves, manifolds, marine flow-control systems, and offshore process equipment, provided the alloy is selected for the actual exposure conditions.
Aerospace and Gas-Turbine Applications
Nickel-based superalloys are fundamental engineering materials for high-temperature aerospace systems.
Casting allows complex shapes to be integrated into a single component while maintaining the performance characteristics required for hot-section service.
Applications may include turbine nozzles, combustion hardware, structural hot-section components, and other specialized gas-turbine parts.
The exact alloy and casting method depend heavily on temperature, stress, oxidation environment, and component geometry.
Energy and Industrial Thermal Equipment
Cast Inconel components can also be used in power-generation systems, industrial furnaces, heat-treatment equipment, combustion systems, and high-temperature processing machinery.
The main advantage is their ability to maintain structural integrity under simultaneous thermal, mechanical, and chemical loads.
9. Limitations of Inconel Casting
Although Inconel casting offers excellent high-temperature strength, corrosion resistance, and complex-geometry capability, it also presents significant manufacturing challenges.
High Material Cost
The first limitation is the relatively high cost of nickel-based superalloys.
Inconel contains large amounts of nickel along with expensive alloying elements such as chromium, molybdenum, niobium, and, depending on the grade, cobalt, tungsten, tantalum, or other additions.
Because of this high material value, casting yield and material utilization are important economic considerations.
Excessive gating and risering, machining allowances, and casting scrap can have a greater cost impact than they would for conventional carbon steel or standard stainless steel castings.
Complex Melting and Casting Requirements
Inconel alloys generally require more controlled melting and pouring conditions than conventional casting alloys.
Their high melting temperatures and complex alloy chemistry make temperature control, atmosphere management, melt cleanliness, and chemical composition control particularly important.
During melting and pouring, inappropriate process conditions can increase the risk of oxidation, inclusions, gas-related defects, or changes in alloy chemistry.
For certain high-performance nickel alloys, vacuum or other controlled-atmosphere melting may therefore be preferred.
Solidification Segregation and Casting Defects
Nickel-based superalloys can exhibit significant microsegregation during solidification because alloying elements partition between the dendritic and interdendritic regions.
Depending on the alloy, undesirable phases such as Laves phases, carbides, or other intermetallic constituents may form.
Common casting defects include:
- Shrinkage porosity
- Gas porosity
- Oxide or non-metallic inclusions
- Hot cracking
- Misruns and cold shuts
- Chemical segregation
- Localized lack of soundness
These defects can reduce ductility, fatigue resistance, corrosion resistance, or creep performance.
Consequently, gating, feeding, mold temperature, pouring conditions, and solidification behavior must be carefully controlled.
Difficult Machinability
Inconel is significantly more difficult to machine than many conventional steels.
Its high strength, low thermal conductivity, and strong work-hardening tendency concentrate heat and cutting forces in the machining zone.
As a result, CNC machining may involve:
- Higher tool wear
- Lower practical cutting speeds
- Greater cutting-force requirements
- More stringent workholding and machine rigidity
- Increased machining time and tooling cost
For this reason, the casting design should be optimized to produce the final geometry as close to net shape as practical, while machining is reserved for critical dimensions, sealing surfaces, threads, bores, and other functional features.
Greater Heat-Treatment Complexity
Heat treatment is often essential for achieving the required properties, but the correct cycle is highly dependent on the alloy grade and its intended application.
In precipitation-strengthened alloys, parameters such as solution temperature, cooling rate, aging temperature, and aging time directly influence the resulting microstructure and mechanical properties.
An inappropriate heat-treatment cycle can lead to undesirable phase formation, insufficient strengthening, excessive grain growth, or loss of corrosion resistance.
Therefore, Inconel castings require alloy-specific thermal processing rather than a generic heat-treatment procedure.
Higher Inspection Requirements
Because Inconel castings are often used in high-temperature, high-pressure, or corrosive service, internal and surface integrity may be subject to strict acceptance criteria.
Inspection can include chemical analysis, dimensional inspection, penetrant testing, radiography, ultrasonic testing, CT scanning, metallographic examination, and mechanical-property verification.
The required inspection level increases manufacturing time and cost, but it is often essential for demonstrating casting integrity and ensuring reliable service performance.
Higher Overall Manufacturing Cost
The combination of expensive raw material, specialized melting equipment, complex casting control, heat treatment, difficult machining, and extensive inspection makes Inconel castings considerably more expensive than many conventional metal castings.
Therefore, Inconel casting is generally most justified when the component requires a combination of properties that lower-cost alloys cannot reliably provide.
For less demanding applications, stainless steel, alloy steel, nickel-iron alloys, or other lower-cost materials may provide a more economical solution.
10. Choose LangHe Industry for Inconel Casting
LangHe Industry is an ISO-certified manufacturer providing custom investment casting and CNC machining solutions for complex metal components.
For Inconel applications, LangHe can integrate DFM analysis, casting process development, alloy selection, precision investment casting, heat treatment, CNC machining, surface finishing, and quality inspection into a coordinated manufacturing workflow.
The engineering approach focuses on matching the manufacturing process to the actual requirements of the component.
For complex Inconel castings, this includes evaluating wall thickness, section transitions, gating and feeding, machining allowances, datum structures, heat-treatment requirements, and inspection requirements before production.
Critical functional features can then be CNC machined to the required dimensional and surface specifications.
LangHe supports custom production for prototype, small-batch, and repeat industrial components, with the final process defined according to the selected Inconel grade, component geometry, service conditions, and applicable quality requirements.
This integrated casting-and-machining approach is particularly valuable for customers seeking a finished Inconel component rather than a raw casting alone.
11. Conclusion
Inconel alloys occupy an important position among high-performance engineering materials because they combine high-temperature strength, oxidation resistance, corrosion resistance, and long-term structural stability.
Their performance comes from carefully controlled nickel-based metallurgical systems containing chromium and selected strengthening elements such as molybdenum, niobium, aluminum, and titanium.
For complex components, casting provides an effective route to transform these high-performance alloys into near-net-shape parts while reducing the machining required for difficult-to-cut nickel alloys.
Investment casting is particularly valuable for intricate geometries, while vacuum investment casting is suitable when tighter control of melt cleanliness and atmospheric contamination is required.
Centrifugal and sand casting have more specialized applications based on component geometry and size.
However, successful Inconel casting depends on much more than selecting the alloy.
Melting practice, mold design, solidification control, heat treatment, machining, and inspection must work together to achieve the required final properties.
When these factors are properly controlled, cast Inconel components can provide reliable performance in some of the most demanding chemical, thermal, energy, marine, and high-temperature industrial applications.
FAQ
What is the difference between Inconel and stainless steel?
Inconel alloys are nickel-chromium-based superalloys with higher nickel content and superior high-temperature strength, oxidation resistance, and corrosion resistance compared with stainless steels.
Stainless steels are iron-based alloys with at least 10.5% chromium.
Can Inconel alloys be cast?
Yes. Inconel alloys are commonly cast by investment casting, vacuum investment casting, centrifugal casting, and sand casting.
Casting is often preferred for complex shapes and for alloys that are difficult to machine.
Which Inconel grade is best for high-temperature casting?
It depends on the application. Inconel 718 is widely used for high-strength, moderate-temperature service.
Inconel 625 offers excellent corrosion resistance and good high-temperature strength.
For the hottest turbine sections, cast alloys such as Inconel 738 or single-crystal nickel-based superalloys are often used.
Is Inconel magnetic?
Most Inconel alloys are austenitic and essentially non-magnetic in the annealed condition. Some grades may become slightly magnetic after cold working or certain heat treatments.
How much does Inconel casting cost?
Inconel castings are more expensive than carbon steel or stainless steel castings due to raw material cost, melting complexity, and post-processing requirements.
The final price depends on alloy grade, part size, complexity, quantity, inspection level, and delivery requirements.
Can cast Inconel components be welded?
Many cast Inconel components can be welded, but procedures must be carefully controlled.
Precipitation-hardened grades such as 718 require proper pre-heat, filler selection, and post-weld heat treatment to avoid cracking.
What is HIP in Inconel casting?
HIP stands for Hot Isostatic Pressing. It uses high temperature and high gas pressure to close internal porosity in castings, improving density, fatigue life, and mechanical properties.