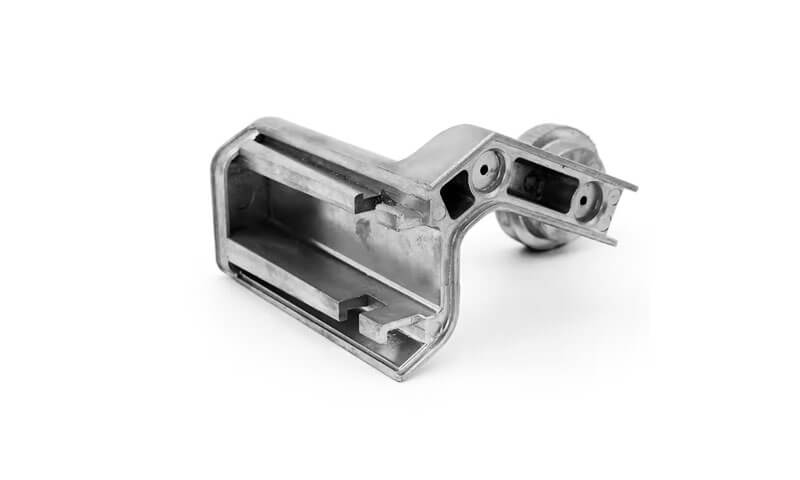
铝铸造是一种实用的制造解决方案,用于生产具有复杂几何形状的轻质金属部件, 综合功能特点, and high material efficiency.
Compared with machining a component entirely from billet, casting can establish much of the required geometry in the mold, reducing material removal and machining time.
Depending on part geometry, 生产量, 维度要求, 和机械性能, manufacturers can select from 重力铸造, 低压铸造 (LPDC), 高压铸造 (HPDC), 投资铸造, 和砂型铸造.
LangHe Industry approaches custom aluminum casting as an integrated manufacturing process rather than an isolated foundry operation.
Our workflow can incorporate engineering review, casting process selection, tooling and pattern development, aluminum melting, 铸件, 热处理,
数控加工, 表面饰面, 和质量检查, allowing customers to develop components from prototype quantities through repeat production.
1. 什么是铝铸件?
铝铸件 is a manufacturing process in which molten aluminum alloy is introduced into a mold cavity and allowed to solidify into a predetermined geometry.
Depending on the required component, 生产量, 维度的准确性, 和机械性能, the mold may be made from bonded sand, ceramic materials, or reusable metal tooling.
The fundamental advantage of aluminum casting is its ability to transform a relatively complex three-dimensional design into a near-net-shape component in a single primary forming operation.
Features that would require extensive machining or assembly when manufactured from solid stock—such as ribs, 老板, curved walls, 住房, and internal cavities—can often be incorporated directly into the casting.
The Basic Aluminum Casting Sequence
Although different casting technologies use different equipment and tooling, the fundamental manufacturing sequence is similar:
Alloy selection → mold/tooling design → melting → melt treatment → mold filling → solidification → demolding → cleaning → heat treatment → machining → finishing → inspection
2. Core Casting Process Technologies at LangHe Foundry
LangHe Foundry uses a diversified aluminum casting platform to match the manufacturing process to the part geometry, 生产量, 维度要求, 表面饰面, and mechanical-property targets.
No single casting method is suitable for every aluminum component. The primary processes include gravity die casting, 低压铸造, 高压铸造, 投资铸造, 和砂型铸造.
重力铸造 (永久模具)
重力铸造, 也称为 永久模具铸件, 使用可重复使用的金属模具, typically manufactured from cast iron or steel.
Molten aluminum is introduced into the cavity primarily by gravity, while mold coatings and controlled mold preheating are used to manage release and solidification.
Because the metal mold extracts heat relatively efficiently, gravity die casting can produce a finer and more uniform casting structure than many conventional sand-casting conditions.
It also provides better surface finish and dimensional consistency.

主要特征包括:
- Good mechanical properties resulting from relatively controlled solidification.
- Good surface finish and dimensional consistency compared with sand casting.
- Reusable tooling suitable for medium- 进行大量生产.
- Lower tooling investment than high-pressure die casting in many applications.
- Longer cycle times than HPDC but generally shorter than conventional sand casting.
Typical applications include pump housings, engine and machinery brackets, 电气外壳, 车轮, and structural aluminum components
The main limitations are geometric. 非常薄的墙, 深层削减, and highly intricate features can be more difficult to produce than with HPDC, while cycle times are generally longer because filling is driven primarily by gravity.
低压铸造 (LPDC)
低压铸造 fills the mold from below by applying controlled gas pressure to a sealed holding furnace.
The molten aluminum rises through a stalk or riser tube into the die cavity, with typical filling pressures commonly in the approximate range of 0.1–1 bar
Unlike gravity filling, LPDC provides controlled upward metal flow and can maintain pressure during solidification.
This can improve feeding and reduce the tendency toward certain shrinkage defects when the process is properly designed.
LPDC is particularly suitable for components where 内部声音, 结构完整性, 和一致的机械性能 很重要.
The process is widely associated with aluminum wheels and can also be used for selected housings, 制动组件, and structural castings.
Its main advantages include:
- 受控, relatively low-turbulence filling
- Good metal utilization
- 高重复性
- Good internal quality for suitable designs
- Suitability for medium- 进行大量生产
Its limitations include slower cycle times than HPDC and a narrower range of practical geometries.
Equipment and tooling requirements are also more specialized than conventional sand casting.
高压铸造 (HPDC)
高压铸造 injects molten aluminum into a reusable steel die at high velocity and pressure.
Typical die-casting pressure levels can reach approximately 700–1,400 bar, depending on machine design, 合金, and process stage.
HPDC is optimized for high-volume production of complex, 薄壁组件.
Rapid filling allows intricate features, 肋骨, 老板, and integrated mounting structures to be formed with limited secondary machining.
Under suitable conditions, wall sections around 0.8 mm or slightly thicker may be achievable in selected areas, but the practical minimum depends strongly on alloy, projected area, 流长, 模具设计, and thermal conditions.

典型的应用包括:
- Automotive transmission and motor housings
- Engine and structural covers
- 电子外壳
- Industrial housings
- Complex lightweight structural components
The major advantages are high productivity, 优异的尺寸重复性, 良好的表面饰面, and extensive feature integration.
The main limitations are the high cost of steel dies and the potential for gas porosity and trapped air caused by high-speed filling.
This can also restrict the suitability of conventional HPDC for certain heat-treatment or pressure-tight applications unless specialized processes are used.
熔模铸造
熔模铸造, 或失去的蜡铸, uses a wax pattern to create a ceramic shell mold.
The wax pattern is coated with successive layers of refractory ceramic, after which the wax is removed and the ceramic shell is fired before molten aluminum is introduced.
The process is especially valuable when the component has complex three-dimensional geometry, 细节, 薄部分, or internal features that are difficult to reproduce economically using conventional sand or permanent-mold processes.
Investment casting can provide good surface reproduction and dimensional accuracy.
Representative surface finishes may be in the range of approximately 125–250 microinches RMS, 取决于合金, 壳系统, 和工艺条件.
关键优势包括:
- Complex geometry and high design freedom
- 良好的维度准确性
- Good surface reproduction
- 近网状生产
- 广泛的合金选择
Typical applications include precision industrial components, aerospace-related hardware, medical equipment components, and other complex aluminum parts.
The primary limitations are higher tooling and processing costs compared with conventional sand casting and generally lower productivity for very large production volumes.
沙子铸造 (树脂 & 绿沙)
沙子铸造 uses a disposable sand mold to create the casting cavity. LangHe Foundry can use different sand systems, 包括 green sand and resin-bonded sand, according to part size, 几何学, 生产量, 和尺寸要求.
Green sand uses a moisture-containing molding system, while resin-bonded sand uses a chemically cured binder system.
Resin sand can provide better control for complex molds and cores, whereas green sand is widely used for economical general-purpose production.
Sand casting offers the greatest flexibility for large components and low- 进行中体积生产.
Tooling costs are generally much lower than those of permanent molds or HPDC dies, and the process can accommodate relatively large and complex components.
典型的应用包括:
- Large pump and valve housings
- Machine bases and housings
- Industrial equipment components
- Prototype castings
- Large custom aluminum structures
Its main limitations are rougher surface finish, lower dimensional accuracy, and greater machining requirements compared with die casting or investment casting.
Process Selection at LangHe Foundry
The appropriate aluminum casting process is determined by the part design and production requirements, rather than by casting method alone.
Gravity die casting and LPDC are well suited to applications requiring controlled solidification and consistent properties; HPDC is optimized for high-volume, complex thin-wall production;
investment casting addresses intricate precision geometries; and sand casting remains highly effective for large or low-volume components.
This process flexibility allows Langhe Foundry to balance tooling investment, 生产效率, 维控制, 表面质量, and mechanical requirements for each aluminum casting application.
3. Materials Science & Aluminum Alloy Metallurgy
Alloy selection is one of the most important decisions in aluminum casting because it directly affects castability, 机械强度, 耐腐蚀性, 可加工性, 热处理反应, 和使用温度.
常见的铝制铸造合金
The most widely used casting alloys are based primarily on al-si, al-si-mg, and Al-Si-Cu systems.
Silicon improves fluidity and filling behavior, magnesium enables precipitation hardening, while copper can increase strength and improve machinability but generally reduces corrosion resistance.
| 合金 | Typical Alloy System | 关键特征 | 典型的应用 |
| A356 | al-si-mg | 出色的铸造性, 耐腐蚀性, and good strength after T6 treatment | 住房, 结构部件, 汽车组件 |
| A357 | al-si-mg | Higher Mg content than A356, providing higher heat-treated strength | High-strength structural castings, demanding engineering components |
| A380 | al-si-cu | Excellent die-filling ability, good strength and machinability, widely used for die casting | 汽车零件, 住房, 括号, 工业组件 |
| ADC12 | Al-Si-Cu-Fe | 出色的流动性, good dimensional stability and productivity in HPDC; widely used for complex thin-wall parts | 汽车住房, 电机零件, electronic and industrial enclosures |
A383 |
al-si-cu | High fluidity and good resistance to hot cracking; suitable for complex die-cast geometries | Complex die-cast housings and structural components |
| A413 | al-si | High silicon content, excellent fluidity and pressure tightness | 液压成分, 住房, 薄壁铸件 |
| A390 | High-Si Al alloy | High wear resistance and good dimensional stability, but more difficult to machine | 发动机组件, 泵, 耐磨零件 |
| A206 | 铝铜 | High strength and fatigue performance after heat treatment, with lower castability than Al-Si alloys | Structural and high-strength engineering components |
Heat-Treatable vs Non-Heat-Treatable Alloys
Heat-treatable alloys derive a significant portion of their strength from controlled metallurgical reactions after casting. A356, A357, and A206 are representative examples.
A typical T6 route consists of solution heat treatment, 快速淬火, 和人工衰老, with exact temperatures and holding times determined by the alloy specification, casting section thickness, and required properties.
Non-heat-treatable alloys (A443, A518) rely primarily on their as-cast microstructure and alloy chemistry for strength.
Their performance can still be improved through control of melt quality, 谷物结构, 铸造缺陷, 和冷却条件, but they do not obtain the same precipitation-hardening response as A356 or A357.
This distinction is particularly important in high-pressure die casting.
Although some die-casting alloys have heat-treatment potential, conventional HPDC parts may contain entrapped gas and porosity that can expand or cause blistering during high-temperature solution treatment.
为此原因, alloys such as A380 and ADC12 are commonly used in the as-cast condition or with selected low-temperature aging treatments, depending on the component and process design.
4. Engineering Integration: DFM & Simulation Capabilities
Custom aluminum casting is most reliable when manufacturability is addressed before tooling is produced.
LangHe Foundry treats DFM as an engineering stage rather than a final production check.
The purpose is to transform a customer’s CAD model into a geometry that can be filled, 固化, 热处理, 加工, and inspected consistently.
Design for Manufacturability Review
The engineering review evaluates the part from both product and foundry perspectives.
Important areas include:
- Wall thickness and transitions
- Draft requirements
- Fillets and radii
- 肋骨和老板
- Core accessibility
- Gating and feeding
- 铸造收缩率
- 机械加工余量
- Datum strategy
- Clamping and inspection surfaces
例如, a sudden transition from a thin wall to a very thick boss can create a local thermal concentration.
The thicker region may remain liquid longer during solidification and become vulnerable to shrinkage porosity.
A small geometric modification—such as adding a fillet, reducing unnecessary mass, or improving a transition—can therefore improve casting quality without changing the component’s basic function.
Wall Thickness and Section Transitions
Uniformity of section thickness is one of the most useful general principles in aluminum casting.
Large differences in wall thickness can produce:
Different cooling rates → different solidification times → thermal imbalance → increased defect risk
This does not mean every casting must have perfectly uniform walls. Functional requirements often require ribs, 老板, 安装垫, and other local features.
The engineering objective is to control these changes through gradual transitions and appropriate thermal design.
Gating and Feeding Design
The gating system controls how molten metal reaches the mold cavity, while the feeding system compensates for contraction during solidification.
The engineering review considers:
- Gate location
- Runner dimensions
- Filling sequence
- Riser position
- Local hot spots
- 方向固化
- Overflow and venting where applicable
A properly designed system can reduce turbulence, 改善填充, and provide better feeding of sections likely to develop shrinkage.
Mold-Filling and Solidification Simulation
For complex or high-value parts, numerical simulation can be used to evaluate the proposed casting before physical trials.
Casting simulation software can model mold filling, 传热, 凝固, and shrinkage-related behavior.
Commercial platforms such as MAGMASOFT and ProCAST are examples of tools used in industrial foundry engineering.
Simulation can help identify:
| Simulation Area | 工程目标 |
| Filling Pattern | Identify incomplete filling and unfavorable flow paths |
| Temperature Distribution | Evaluate thermal balance during filling |
| Solidification Sequence | Determine where solidification occurs first and last |
| Hot Spots | Identify regions with elevated shrinkage risk |
| Porosity Prediction | Identify areas potentially susceptible to internal shrinkage |
| Gating/Riser Design | Optimize metal delivery and feeding |
| Process Alternatives | Compare different process or geometry solutions before trials |
Simulation is a predictive engineering tool, not a substitute for production validation.
Actual casting results still depend on melt condition, 模具温度, machine settings, operator control, 和工艺稳定性.
CAD/CAM集成
Once the casting design is validated, CAD/CAM data can be used throughout tooling and machining development.
The same digital model can support:
Casting geometry → Tooling design → CNC programming → Inspection
This reduces the risk of discrepancies between the original drawing, the casting model, and the final machining program.
For custom production, digital data continuity is particularly useful when the customer makes engineering revisions. Changes can be evaluated before tooling or machining instructions are released.
Datum Strategy for Castings
The casting should be designed with a logical machining datum strategy. Critical machining surfaces should be referenced to stable and repeatable features of the casting.
This is particularly important for components containing:
- 轴承孔
- Mounting holes
- 密封面
- Shaft interfaces
- Multiple related machining features
Poor datum selection can create a chain of dimensional errors even when each individual machining operation appears acceptable.
The objective is to control the relationship between features, not simply the dimension of each feature in isolation.
5. Advanced Post-Processing, 加工, 和表面饰面
Casting establishes the basic geometry of an aluminum component, but additional processing is often required to achieve the specified mechanical properties, 维度的准确性, 表面状况, 和功能性能.
At LangHe Foundry, post-processing is selected according to the alloy, 铸造方法, 零件几何, 公差要求, and final application.

热处理
Heat treatment is primarily applied to heat-treatable aluminum casting alloys such as A356 and A357.
The most common conditions include T4 and T6, while selected alloys and applications may use other temper conditions.
A typical T6治疗 consists of three stages:
- 溶液热处理 to dissolve suitable alloying constituents into the aluminum matrix.
- 淬火 to retain the supersaturated solid solution.
- 人工衰老 to promote controlled precipitation and increase strength and hardness.
For A356-type alloys, solution treatment is commonly carried out at approximately 530–545°C, followed by rapid quenching and artificial aging often in the range of 150–180°C.
Exact temperatures, holding times, and cooling conditions must be established according to the alloy specification and casting geometry.
Heat treatment must also consider casting porosity and dimensional stability. Excessive heating of pressure-die-cast components with significant entrapped gas can lead to dimensional changes or surface blistering.
所以, the appropriate temper and heat-treatment route should be determined together with the casting process.
CNC Machining of Aluminum Castings
Precision machining is used to convert selected casting surfaces into functional features with controlled dimensions and positional relationships.
典型的操作包括 facing, 铣削, 钻孔, 无聊的, 窃听, 旋转, 线程, 开槽, and undercutting.
Machining is particularly important for:
- Bearing seats and precision bores
- 密封面
- Mounting faces
- 螺纹孔
- Shaft and coupling interfaces
- Dimensional reference surfaces
A key consideration is the relationship between casting geometry and machining datums.
Functional surfaces should be machined from stable reference features so that concentricity, 并行性, perpendicularity, and positional accuracy can be controlled consistently.
For appropriately designed aluminum castings, dimensional machining tolerances of around ±0.05毫米 can be used as a practical reference for many features, while tighter tolerances may be achievable on selected dimensions under controlled CNC conditions.
Actual capability depends on part size, 几何学, 合金, 热处理条件, 机器能力, 及检验要求.
表面处理
Surface finishing can improve appearance, remove casting residues and burrs, and provide additional corrosion or wear protection.
The selected treatment should be compatible with the aluminum alloy and the required service environment.
| 表面处理 | 主要目的 | 典型的应用 |
| 射击 | 删除规模, 残留物, and loose surface material; produces a uniform texture | General industrial castings |
| 振动整理 | Deburring and edge smoothing | Small and medium components |
| 阳极氧化 | Forms a controlled aluminum oxide layer for corrosion resistance and appearance | 住房, 封面, consumer and industrial components |
| 粉末涂料 | Provides a durable decorative and protective coating | Exterior and industrial parts |
绘画 |
Provides color and additional environmental protection | Machinery and equipment components |
| 镀铬转化涂层 | Improves corrosion protection and can maintain electrical conductivity | Electrical and industrial enclosures |
| 激光标记 | Permanent identification and traceability | Part numbers, QR codes, 徽标, batch information |
Assembly and Functional Testing
For components supplied as finished assemblies, post-processing may extend beyond machining and surface treatment.
Depending on the product, services can include insert installation, bearing pressing, 紧固, sub-assembly, dimensional verification, and protective packaging.
Pressure-containing aluminum castings may also require leak testing.
Air-pressure or water-pressure testing is commonly selected according to the component design and customer specification, while helium testing may be used where substantially higher leak sensitivity is required.
Test pressure, stabilization time, allowable leakage, and acceptance criteria should always be defined by the applicable drawing or engineering specification.
The objective of post-processing is not simply to improve appearance.
A properly controlled sequence of heat treatment, 数控加工, 表面饰面, 集会, and functional testing ensures that the cast component meets its final dimensional, 机械的, 及服务要求.
6. 质量保证 & Compliance Standards
Quality control is essential for aluminum castings because casting defects, 尺寸变化, heat-treatment inconsistencies, and machining errors can directly affect the performance of the finished component.
At LangHe Foundry, quality assurance should cover the complete manufacturing chain, from raw material and melt control to casting, 热处理, 加工, 表面饰面, 和最终检验.
Material and Chemical Composition Control
The first stage is verifying that the selected alloy conforms to the required specification.
Chemical composition is checked using appropriate material-analysis equipment, with particular attention to the elements that strongly influence casting behavior and mechanical properties, 包括 和, 毫克, 铜, 铁, Mn, 和锌.
For production orders, material identification and batch traceability help ensure that the alloy used in the casting corresponds to the approved specification.
Casting Process Control
Casting quality depends heavily on controlling the process rather than relying only on final inspection.
Important parameters include melt temperature, 模具温度, 灌装条件, pouring or injection parameters, 脱气, 熔体清洁度, 和凝固行为.
适用于复杂铸件, process simulation can also be used during engineering development to identify potential filling problems, 热点, and shrinkage-prone areas before production tooling is finalized.
Heat Treatment and Mechanical Verification
For heat-treatable alloys, heat-treatment records should be controlled according to the specified temper condition.
A356-T6, 例如, requires controlled solution treatment, 淬火, and artificial aging to achieve its specified mechanical performance.
The acceptance criteria should be based on the applicable alloy specification, 绘画, purchase order, or customer technical standard rather than a general value applied to every casting.
Dimensional and Surface Inspection
After casting and machining, critical dimensions are inspected using calibrated measuring equipment.
Depending on part complexity, inspection may include calipers, 微米, 仪表, 高度尺, CMM, optical inspection systems, and specialized fixtures.
Surface inspection covers casting appearance, 加工标记, 毛刺, 裂缝, coating condition, and other customer-specified requirements.
Where necessary, X射线/CT, 染料渗透剂, or other nondestructive testing methods can be incorporated according to the component’s risk level and specification.
Compliance and Traceability
Custom aluminum castings may need to comply with ASTM, 在, 从, GB, or customer-specific material and dimensional standards, depending on the destination market and application.
The applicable standard should always be defined at the quotation and drawing-review stage.
Traceability can extend from raw-material batch → melt/heat → casting lot → heat treatment → machining → inspection → final shipment.
This is particularly important for pressure-containing, safety-related, and repeat-production components.
LangHe Foundry is an ISO认证制造商, supporting a structured quality-management approach throughout custom casting production.
7. Custom Aluminum Casting vs. Aluminum Machining: 更好?
Custom aluminum casting and CNC machining are not competing solutions in every application.
They address different manufacturing requirements, and in many cases the most effective solution is a combination of casting and machining.
| 因素 | Custom Aluminum Casting | CNC Machining from Aluminum |
| Basic principle | Molten aluminum is formed into the required geometry | Material is removed from billet, 盘子, or bar stock |
| 复杂的几何形状 | Excellent for integrated shapes, 肋骨, 老板, and internal features | More limited by tool access and material removal |
| 工具 | 需要图案, 模具, 或死亡 | Generally requires no casting mold |
| 初始工具成本 | 更高, especially for die casting | Lower for prototypes and low volumes |
| 高体积生产 | Well suited to repeat production | Can become more time- and material-intensive |
尺寸精度 |
良好, followed by machining where necessary | Generally higher on directly machined features |
| 物质效率 | Near-net-shape production can reduce machining stock | Significant material is removed from solid stock |
| 表面状况 | Depends on casting method and alloy | Directly controlled by cutting parameters and tools |
| Prototype flexibility | 一般, depending on tooling method | 出色的 |
| Typical strategy | Cast the main body, then machine critical features | Machine the complete part from stock |
A Combined Casting + CNC Strategy
For many industrial components, the most practical solution is not casting 或者 加工, 但:
Design → Aluminum Casting → Heat Treatment → CNC Machining → Surface Finishing → Inspection
This approach separates the two manufacturing functions effectively:
- 铸件 provides geometric complexity and near-net shape.
- 数控加工 provides precision.
- 热处理 develops required mechanical properties where applicable.
- 表面饰面 provides corrosion protection and appearance.
- 检查 verifies the finished part against the drawing.
The correct process therefore depends on geometry, 合金, annual quantity, 宽容, 表面要求, tooling budget, 和总制造成本, rather than on one process being universally superior.
8. Strategic Procurement: Why Choose LangHe Foundry for Custom Aluminum Casting?
Selecting a custom aluminum casting manufacturer is a strategic decision that affects quality, 成本, 交货时间, and supply chain reliability.
Langhe Foundry offers a combination of capabilities that make it a strong choice for custom aluminum casting projects.
Diversified process portfolio.
LangHe operates gravity die casting, 低压铸造, 高压铸造, 投资铸造, 和砂型铸造.
This allows the foundry to select the optimal process for each application rather than forcing a single process to fit every part.
Engineering integration.
LangHe’s engineering team provides DFM feedback, 模拟, 和过程优化. This reduces development time, improves first-time quality, and lowers total cost.
In-house machining and finishing.
LangHe offers CNC machining, 热处理, 阳极氧化, 粉末涂料, 绘画, 和组装. This reduces lead times, controls quality, and simplifies supply chain management.
质量系统.
LangHe maintains a documented quality system with material certification, 维度检查, NDT, 和完整的可追溯性. This is essential for automotive, 航天, 医疗的, and other critical applications.
Production flexibility.
LangHe can produce prototypes, 小批次, and high-volume production runs. The foundry’s capacity and process control allow it to meet demanding delivery schedules.
Industry experience.
LangHe serves customers in automotive, 航天, 活力, 电信, 医疗的, 工业的, and consumer product industries. This experience informs every project.
A Single Manufacturing Partner for Custom Aluminum Castings
LangHe Foundry’s value lies in integrating casting technology, engineering support, 数控加工, 表面饰面, 检查, and supply coordination into one manufacturing workflow.
This reduces the need to manage separate suppliers for individual production stages and provides a clearer technical interface from drawing review to finished part.
For buyers evaluating a custom aluminum casting supplier, the key considerations are therefore not only unit price, but also process capability, engineering support, quality consistency, 生产灵活性, 和总拥有成本.
LangHe’s integrated approach is designed to address these requirements from initial development through repeat production.
9. 结论
Custom aluminum casting is a versatile and cost-effective manufacturing process for producing complex, 轻的, 和耐用组件.
The choice of casting process—gravity die, 低压, 高压, 投资, or sand—depends on geometry, 体积, 宽容, 表面饰面, and mechanical property requirements.
Langhe Foundry offers a comprehensive casting platform, engineering support, in-house machining and finishing, and a strong quality system.
This combination allows the foundry to deliver custom aluminum castings that meet the most demanding specifications while controlling cost and lead time.
Whether the application is an automotive housing, an aerospace bracket, an electronic enclosure, or an industrial pump body, the right casting partner can make the difference between a component that performs reliably and one that fails prematurely.
Langhe行业 is positioned as such a partner, offering the technical depth, production capability, and quality assurance needed for custom aluminum casting projects.
常见问题解答
Is ADC12 suitable for custom aluminum casting?
是的. ADC12 is widely used for high-pressure die casting because of its good fluidity, 维稳定性, and suitability for complex components.
It is commonly used for housings, 括号, 电机组件, and other industrial and automotive die-cast parts.
Can aluminum castings be heat treated?
是的, but the applicability depends on the alloy and casting process. A356 and A357, 例如, are commonly supplied in heat-treated conditions such as T6.
Conventional high-pressure die-cast alloys such as ADC12 require additional consideration because entrapped gas and porosity can affect their response to high-temperature treatment.
Can LangHe provide machining after aluminum casting?
是的. Custom aluminum castings can be combined with CNC machining for bores, 线程, 密封表面, 安装接口, and other precision features, followed by inspection and suitable surface finishing.
What is the difference between gravity die casting and high-pressure die casting?
Gravity die casting pours molten aluminum into a metal mold under gravity, producing good mechanical properties and surface finish at moderate volumes.
High-pressure die casting injects molten aluminum at high pressure, 产生复合物, thin-wall parts at high volumes with excellent dimensional accuracy.
What is low-pressure die casting used for?
Low-pressure die casting is used for symmetric, high-integrity parts such as automotive wheels, 气缸盖, and brake calipers. It offers excellent internal quality and high material yield.