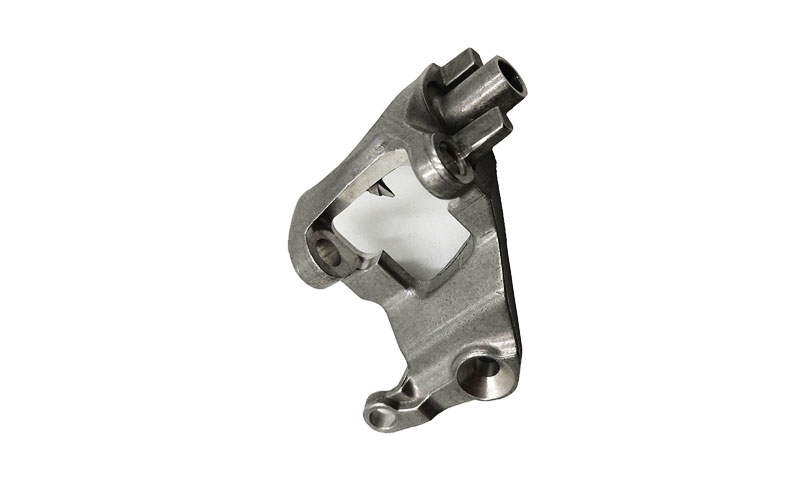
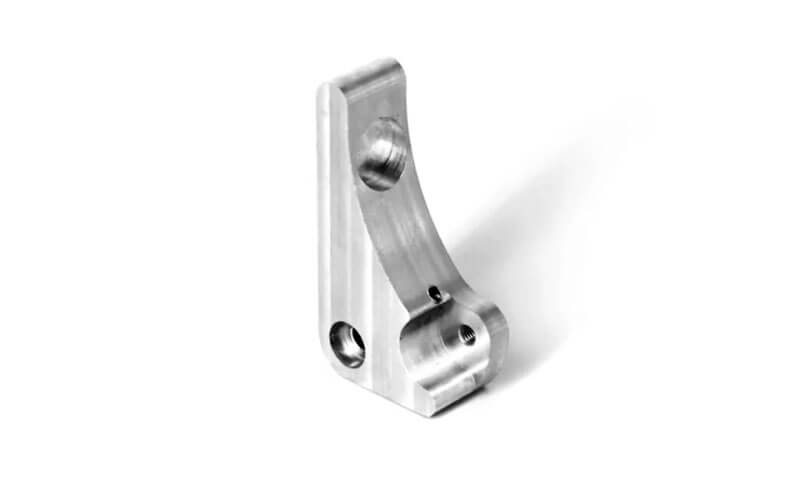
选择之间 precision cast aluminum and cast steel is not simply a matter of comparing weight or material price.
在 投资铸造, the difference between these two material families affects almost every stage of production—from alloy melting and shell preparation to gating, 进食, 热处理, 加工, 和最终检验.
After years of working with precision casting processes, I have found that many casting problems occur when a process developed for steel is simply transferred to aluminum without changing the underlying approach.
Aluminum alloys have lower density, higher thermal conductivity, strong oxidation behavior, and different solidification characteristics.
铸钢, 同时, demands higher pouring temperatures and generally places greater thermal and mechanical demands on the ceramic shell and gating system.
I will cover the essential differences, the melting and pouring challenges, the role of filtration and modifiers, the treatment of return materials, and the decision criteria that should drive material selection.
Where I can, I will share data from my own experience and from the shops I have worked with.
1. 精密铸铝与铸钢: The Fundamental Difference
The most obvious difference is density. Aluminum alloys typically have a density of around 2.6–2.8 克/立方厘米, while carbon and alloy steels are generally around 7.8–7.9 g/cm³.
A comparable aluminum casting can therefore be dramatically lighter than a steel casting.
But weight is only the beginning.
Aluminum also has a much lower melting temperature, 通常在周围 600–660°C depending on alloy, whereas steel is generally poured at temperatures well above 1,500°C.
This completely changes the casting environment. Aluminum is more sensitive to hydrogen absorption and oxide-film formation, while steel places much greater demands on shell refractoriness, 热电阻, 和门控设计.

From a foundry perspective, I would summarize the difference this way:
Aluminum casting is often a battle against oxidation, 氢, 进食, 和清洁; steel casting is more often a battle against temperature, 填充, 凝固, and thermal stress.
Neither material is inherently better. They simply require different process thinking.
2. Key Material Differences Between Precision Cast Aluminum and Cast Steel
Before comparing applications, it is important to understand the fundamental metallurgical differences between aluminum and steel.
在熔模铸造中, these differences directly determine how the foundry approaches melting, 壳制备, 门控, 进食, 过滤, 和浇注.
| 性能特性 | 精确 铸造铝 | 精确 铸钢 |
| 融化 / 浇注温度 | Typically around 700–780°C, alloy and process dependent | Typically around 1,550–1,650°C for pouring, grade and process dependent |
| 密度 | Approximately 2.6–2.8 g/cm³ | 大约 7.8 g/cm³ |
| 流动性 | 一般优秀; well suited to thin walls and fine details | 良好, but requires careful thermal management and often higher shell temperatures |
| Linear solidification shrinkage | Approximately 1.0–1.3% for typical alloys | Approximately 0.5–0.7% |
| 导热率 | 高的; heat is transferred rapidly | Much lower; heat is retained longer |
Oxidation tendency |
很高; Al₂O₃ film forms rapidly on exposed molten metal | 重要的, with slag and oxide formation requiring control |
| Hydrogen sensitivity | 高的; moisture can introduce dissolved hydrogen and porosity | Relatively low compared with aluminum |
| Surface-detail reproduction | Excellent when the melt and shell are well controlled | 良好; strongly dependent on shell quality and pouring conditions |
3. Why Precision Cast Aluminum Is Attractive
Precision cast aluminum is particularly valuable when weight reduction and complex geometry are major design objectives.
Because aluminum alloys are relatively fluid at casting temperatures and have good thermal conductivity, they can reproduce relatively detailed investment-casting geometries effectively.
薄壁, 肋骨, 老板, 腔, and integrated mounting features can often be incorporated into a single casting rather than assembled from multiple components.

The weight advantage is particularly important in transportation and mobile equipment.
Replacing a steel component with aluminum can reduce mass substantially without necessarily sacrificing the required functional performance when the design is properly optimized.
Aluminum also provides good natural corrosion resistance through the formation of a thin oxide layer.
Specific alloys can provide substantially better corrosion resistance than ordinary carbon steel, although alloy selection remains critical.
然而, aluminum’s advantages come with a price: the molten metal is extremely sensitive to contamination and oxide formation.
4. Aluminum Melt Cleanliness and Filtration
From my experience, melt cleanliness is one of the most important factors in precision cast aluminum.
Aluminum can fill a detailed investment casting very well, but if the melt contains oxide films, 浮渣, or dissolved hydrogen, good mold filling alone cannot produce a sound casting.
Oxide Inclusions: The Buoyancy Problem
The relatively low density of aluminum makes inclusion removal more difficult than many people expect.
Molten aluminum has a density of roughly 2.4–2.7 g/cm³, while the density of steel is around 7.8 g/cm³.
更重要的是, 氧化铝 (al₂o₃) formed on the surface of molten aluminum has a density much closer to the aluminum melt than many typical steel inclusions do.
因此, oxide films and fine non-metallic particles can remain suspended in the melt rather than rapidly separating by gravity.
Once the metal enters the mold, these contaminants can become trapped inside the casting, 生产 氧化物夹杂物, bifilms, 表面缺陷, and reduced mechanical reliability.
This is why aluminum investment casting requires deliberate melt-cleanliness control rather than relying on holding time alone.
Ceramic Filtration
Ceramic foam filters are widely used in aluminum investment casting to remove 氧化物膜, 浮渣, and other non-metallic particles.
Filter selection should consider pore size, filter area, metal flow rate, 和铸造几何形状.
For many aluminum castings, 20–30 PPI filters provide a practical starting range, although the final specification should be validated for the specific casting.
The filter should be positioned in a stable section of the gating system and properly preheated to prevent premature metal freezing.
用于关键铸件, multi-stage filtration may be used to improve melt cleanliness without excessively restricting flow.
Hydrogen and Degassing
Hydrogen is another major source of internal defects. Molten aluminum readily absorbs hydrogen from moisture in the atmosphere, 充电材料, and casting equipment.
As aluminum solidifies, hydrogen solubility decreases sharply, increasing the risk of gas porosity and pinholes.
Rotary degassing with argon or nitrogen is commonly used to reduce dissolved hydrogen before pouring.
The treatment parameters should be controlled according to melt condition and production requirements, and the result can be verified using reduced-pressure testing (RPT) or a density-index test.
5. Why Cast Steel Remains the Better Choice for Heavy-Duty Applications
Cast steel has a fundamentally different performance profile.
Its density is much higher than aluminum, but it provides excellent absolute strength, 韧性, 戴阻力, and temperature capability across a broad range of grades.
Carbon steel and alloy steel castings are therefore commonly selected for components subjected to high mechanical loads, 影响, 压力, or elevated operating temperatures.

Steel also offers a very broad range of alloy possibilities. 取决于申请, the foundry can select carbon steel, 低合金钢, 不锈钢, 耐热钢, wear-resistant grades, or other specialized compositions.
For components where 结构强度, 冲击阻力, or elevated-temperature performance is more important than weight, cast steel can be the more appropriate engineering solution.
The disadvantage is equally straightforward: steel is heavy and requires a much more demanding thermal process.
6. Gating System Design: Aluminum and Steel Cannot Be Treated the Same
This is one of the most important differences in investment casting.
A gating system designed for steel cannot simply be copied for aluminum.
Molten aluminum has relatively low density and high thermal conductivity. 更重要的是, it has a strong tendency to form oxide films when the melt surface is disturbed.
Excessive turbulence can fold these films into the metal stream, creating internal defects.
For aluminum investment castings, smooth and controlled filling is therefore essential.
取决于组件, bottom or side feeding concepts can be advantageous because they reduce direct impingement and promote progressive filling.
Steel has a much higher pouring temperature and different flow and solidification behavior.
The gating system must withstand a much greater thermal load while providing adequate feeding and minimizing turbulence, 侵蚀, 以及其他铸造缺陷.
The practical lesson is simple:
Changing the alloy means reconsidering the entire gating and feeding system—not just changing the melting temperature.
7. Feeding and Shrinkage: A Major Difference in Casting Design
Both aluminum and steel alloys undergo solidification shrinkage, but the exact behavior depends strongly on alloy chemistry and the casting’s solidification range.
Aluminum alloys can present substantial feeding challenges, particularly in geometries containing thick sections, 孤立的热点, and abrupt changes in wall thickness.
Because aluminum conducts heat efficiently, local solidification can occur quickly, making feeding-path design particularly important.
恰当的 立管, 发冷, 大门, 部分过渡, and directional solidification must therefore be considered during tooling development.
用于钢, the much higher pouring temperature creates a different thermal environment.
Large thermal gradients and hot spots can remain active for longer, and riser design becomes especially important for preventing shrinkage cavities and porosity.
This is one reason why casting simulation can be valuable before tooling is finalized.
It allows the foundry to evaluate filling behavior, 凝固, 热点, and feeding before committing to production tooling.
8. 融化和倾倒控制
Pouring is the moment of truth in precision cast aluminum. 融化, 脱气, 过滤, 壳制备, and alloy treatment can all be well controlled, but poor pouring practice can introduce defects within seconds.
The objective is to transfer clean molten aluminum into the cavity smoothly, 始终如一地, and with minimum turbulence.
Shell Preparation
浇注前, the ceramic shell should be clean and free from loose particles. Dust, residual ceramic material, and loose sand should be removed with clean air before the shell enters the pouring operation.
During preheating, positioning the pouring cup downward can also help residual particles fall away rather than entering the gating system.
The shell temperature must be reasonably uniform. A large temperature difference between different areas of the shell can change the filling and solidification behavior of the aluminum and contribute to inconsistent casting quality.
浇注温度
For many aluminum investment castings, a pouring temperature around 720 ± 10°C can be used as a practical starting range, but it should not be treated as a fixed value for every casting.
合金成分, 壁厚, filling distance, and casting geometry all affect the appropriate temperature.
I once worked on a casting that developed overheating-related porosity when poured at approximately 720°C.
We reduced the pouring temperature to 690–700°C, and the defect disappeared. The lesson was straightforward: pouring temperature has to match the casting rather than simply follow a standard number.
一般来说, thin and complex sections may require a higher temperature to maintain adequate fluidity, while excessively high temperatures in thick sections can increase the risk of overheating, 与气体相关的缺陷, and other casting problems.
Pouring Stream Control
Molten aluminum oxidizes rapidly when exposed to air, and turbulent pouring increases the opportunity for oxide-film formation and entrainment.
The ladle or pouring lip should therefore produce a 短的, 集中, and continuous metal stream rather than a broken or splashing flow.
The stream should enter the pouring cup smoothly, with unnecessary drops and changes in direction avoided.
This is a small operational detail, but it has a direct influence on melt cleanliness. In aluminum investment casting, every unnecessary splash is a potential source of oxide contamination.
Double Filtration for Critical Castings
对于关键部件, 一个 two-stage filtration arrangement can provide additional control.
A relatively coarse filter can be positioned upstream, such as near the pouring cup or sprue, while a finer filter is placed farther downstream in the runner.
Besides improving inclusion removal, this arrangement can help reduce metal velocity and turbulence before the aluminum reaches the cavity.
The exact filter specification and location should be determined according to the casting weight, 门控设计, and required filling rate rather than applying one configuration to every part.
Shell Temperature and Pouring Time
Investment casting uses a hot ceramic shell, so shell preheating is an important part of pouring control.
取决于合金和铸造几何形状, shell temperatures of approximately 500–600°C 通常使用.
Once the shell is removed from the preheating furnace, the pouring operation should be completed within a controlled time window.
In the production practice described here, keeping the interval within approximately one hour helps prevent excessive shell cooling.
If the shell temperature drops too far, filling and solidification conditions change, particularly for thin or complex sections, and the risk of defects such as pinhole porosity can increase.
The practical principle is simple: control the shell temperature, 浇注温度, pouring stream, and pouring time as one operation.
Aluminum investment casting is particularly sensitive to disturbances during these few seconds, so consistency at the pouring stage is essential for repeatable casting quality.
9. Dimensional Accuracy and Machining
Investment casting is often selected because it can produce relatively complex near-net-shape components with reduced machining requirements.
Precision cast aluminum has an advantage in applications where lightweight geometry and integrated features are important.
Aluminum is also generally easier to machine than many steel grades, although silicon-rich alloys and certain heat-treated conditions can influence tool wear and surface finish.
Precision cast steel generally requires greater machining effort because of its higher hardness and strength, depending on the grade and heat-treatment condition.

For both materials, 然而, the most important factor is often not the machining operation itself but how the casting is designed for machining.
Machining datums, stock allowance, 定位面, 孔, 线程, 密封面, and critical bores should be incorporated into the casting design from the beginning.
A well-designed investment casting should not simply be “cast first and figured out later”.
10. 耐腐蚀性: Choose the Alloy, Not Just the Material Family
It is too simplistic to say that aluminum is corrosion resistant and steel is not.
The actual answer depends on alloy composition, 环境, 表面状况, and exposure.
Many aluminum alloys form a stable oxide layer that provides useful corrosion protection.
Certain aluminum casting alloys are therefore well suited to outdoor equipment, 运输组件, marine-related applications, and general industrial environments.
Steel performance varies much more widely. Ordinary carbon steel requires appropriate protection in many corrosive environments, while stainless and high-alloy cast steels can provide excellent corrosion resistance.
For chemical processing, 船舶设备, 泵, 阀, and other aggressive environments, specific alloy selection is more important than simply choosing aluminum or steel.
11. 决策框架: 何时选择铝与. 钢
The choice between precision cast aluminum and cast steel should be driven by the part’s weight, 机械负载, 工作温度, 腐蚀环境, 维度要求, and overall cost target.
Neither material is universally better. The right choice is the one that provides sufficient performance without adding unnecessary material, 加工, or machining cost.
| 选择因素 | Choose Precision Cast Aluminum When… | Choose Precision Cast Steel When… |
| 重量 | Low mass is a major requirement. Aluminum density is typically around 2.6–2.8 克/立方厘米, making it roughly one-third the density of steel. | Weight is less important than strength, 耐用性, or structural robustness. |
| 力量 & 加载 | Moderate to high strength is required and the design can accommodate aluminum’s lower modulus and strength compared with steel. | High mechanical loads, 影响, 穿, or structural strength are dominant requirements. |
| Operating temperature | Service temperatures are relatively moderate and compatible with the selected aluminum alloy. | The component must maintain mechanical properties at substantially elevated temperatures. |
| 耐腐蚀性 | A suitable aluminum alloy provides the required corrosion resistance, particularly where lightweight construction is also important. | Severe service conditions require a steel grade selected for specific corrosion, 穿, 或高温性能. |
复杂的几何形状 |
薄壁, 轻量级结构, 错综复杂的空腔, and detailed features are important. | Complex geometry is required but the component also needs the higher strength and temperature capability of steel. |
| 热性能 | High thermal conductivity and rapid heat dissipation are beneficial. | Lower thermal conductivity is acceptable or thermal conductivity is not a primary design requirement. |
| 收缩控制 | The foundry has strong control over aluminum’s relatively high solidification shrinkage and associated feeding requirements. | More predictable shrinkage behavior and established steel investment-casting practices are preferred. |
| 融化清洁度 | The manufacturer has reliable hydrogen control, oxide management, 过滤, and clean-melt practices. | The application is less sensitive to the specific melt-cleanliness challenges associated with aluminum. |
加工 |
Lightweight material and relatively good machinability are advantageous for the finished component. | Higher hardness, 力量, or wear resistance is more important than machining efficiency. |
| 典型的应用 | Automotive lightweight components, 住房, 括号, thermal-management parts, equipment components, and other weight-sensitive parts. | Heavy-duty machinery, 工业阀, 结构成分, 耐磨零件, 高负载组件, 和高温应用. |
| Overall selection priority | 减轻重量 + 耐腐蚀性 + 热性能 + 制造效率 | 力量 + 耐用性 + 温度能力 + severe-service performance |
12. How Zhengzhou LangHe Approaches Precision Cast Aluminum and Cast Steel
在 Zhengzhou LangHe, material selection is treated as part of the casting engineering process rather than as a purchasing decision made after the design is complete.
For a new precision casting project, the first step is to understand the component’s actual requirements: 加载条件, 工作温度, 腐蚀环境, 尺寸公差, 加工要求, production quantity, 和预期使用寿命.
From there, the casting process can be developed around the selected alloy.
For aluminum investment castings, particular attention is given to melt cleanliness, 湿度控制, hydrogen management, 过滤, 门控, 进食, 和热处理.
For cast steel, the focus shifts toward shell thermal resistance, 浇注温度, 填充行为, 进食, 合金控制, 和热处理.
Where CNC machining is required, casting and machining can also be considered together.
This allows machining allowances and datum features to be established before tooling is finalized, reducing unnecessary stock and improving the consistency of the finished component.
The objective is not simply to produce a casting that meets the drawing. It is to develop a stable casting-to-finished-part manufacturing route.
13. 结论
The choice between precision cast aluminum and cast steel ultimately comes down to the balance between performance, 重量, 环境, 几何学, 制造业, 和成本.
Precision cast aluminum is particularly attractive when low weight, 耐腐蚀性, 复杂的几何形状, and efficient machining are important.
Precision Cast steel remains the stronger choice for many applications demanding high absolute strength, 冲击阻力, 戴阻力, or elevated-temperature performance.
The manufacturing processes are equally different. Aluminum requires especially careful control of hydrogen, 氧化物夹杂物, 熔体清洁度, 过滤, 门控, and feeding, while steel requires greater attention to high-temperature shell performance, 填充, 热梯度, 进食, 和热处理.
After years of casting work, my view is straightforward: there is no universally better casting material.
The better material is the one whose metallurgical characteristics match the component’s actual service requirements and whose production process can be controlled consistently.
用于精密铸造, good material selection is not the final step before production. It is the starting point of the entire casting process.
常见问题解答
What is the main difference between precision cast aluminum and cast steel?
Aluminum has a lower melting point, 较低的密度, higher thermal conductivity, higher shrinkage, and a much stronger tendency to form oxides and absorb hydrogen.
Steel has higher strength, 较高的温度抗性, and better impact toughness. The casting processes differ in gating, 过滤, melting practice, and mold preparation.
Can a steel foundry easily switch to aluminum casting?
Not easily. The pouring system, 过滤, melting practice, modifier selection, and environmental controls must all be redesigned.
Steel foundries that try to use top-pouring systems for aluminum typically experience severe oxide inclusions and porosity.
Why is filtration more critical for aluminum than for steel?
Aluminum oxide inclusions are nearly neutrally buoyant in aluminum melt, so they do not float out.
Steel inclusions have a greater density difference and can be removed by holding and skimming. Aluminum requires ceramic foam filters for forced removal of inclusions.
What causes pin holes in aluminum castings?
Pin holes are caused by hydrogen dissolved in the melt. Hydrogen comes from the reaction of aluminum with water vapor.
The solubility of hydrogen drops sharply during solidification, so the hydrogen forms bubbles.
Prevention includes controlling humidity, degassing with argon or nitrogen, and limiting pouring time.
What modifiers are used in aluminum-silicon alloys?
钠, 锶, and antimony are the most common modifiers. Sodium is fast-acting but short-lived.
Strontium lasts 6–8 hours but increases pin hole tendency. Antimony offers good fluidity and survives remelting but is cooling-rate sensitive.
Why is iron contamination a problem in aluminum castings?
Iron forms hard, brittle intermetallic compounds that reduce machinability and mechanical properties.
Iron contamination comes from crucibles, 工具, 和涂料. All tools contacting the melt must be coated or made from non-ferrous materials.